What Are the Best Hydraulic Cylinder Parts from China?

Choosing the best Hydraulic Cylinder Parts from China requires more than comparing catalog prices. It demands evidence.

Grand View Research valued the global hydraulic cylinders market at approximately USD 14.13 billion in 2023. Its report projects continued growth through 2030. MarketsandMarkets also identifies construction, agriculture, mining, and material handling as major demand sectors. These figures show opportunity, but they do not prove supplier quality.

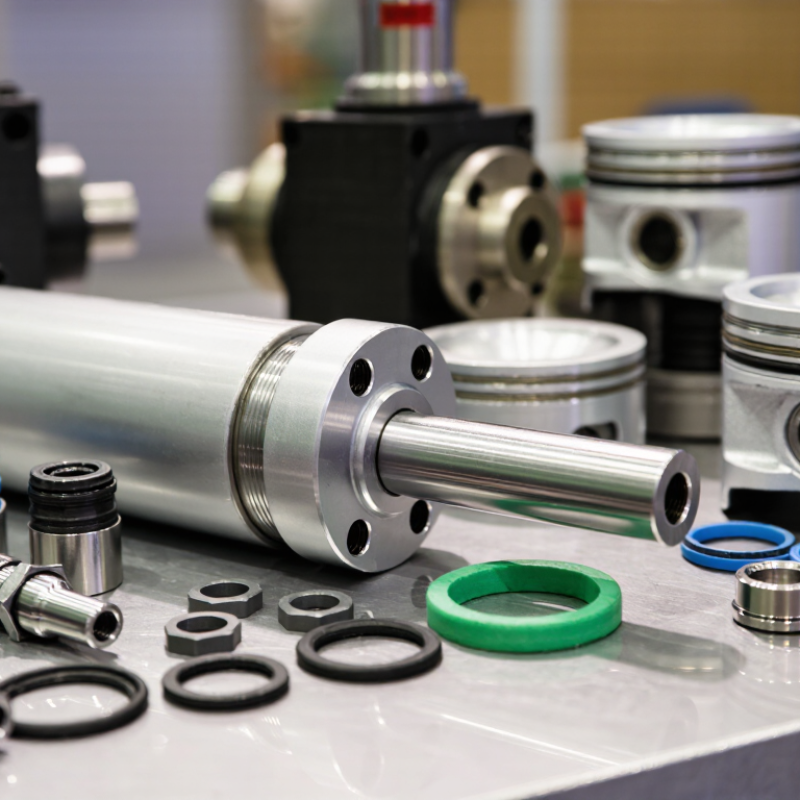
A cylinder can fail through a scratched rod, weak seals, or poor surface treatment. Small defects create expensive downtime. Important components include barrels, pistons, piston rods, glands, guide rings, seals, and mounting accessories. Each part should match pressure, stroke, temperature, fluid, and duty cycle requirements. ISO 6020/2 and ISO 6022 provide useful dimensional and performance references for many metric hydraulic cylinders.

Herbert E. Merritt, author of Hydraulic Control Systems, described hydraulic control as “the art of controlling fluid under pressure.” That principle still matters when selecting Chinese components. Parts must control force consistently, not merely look precise on arrival.

The best supplier can provide material certificates, inspection records, seal specifications, and traceable production data. Ask for rod hardness, chrome thickness, barrel honing results, and leakage-test methods. Request samples before approving large orders.

A low price can look convincing.

It may also hide inconsistent steel, weak quality control, or unclear tolerances. Some supplier claims require independent verification. No factory is perfect, and this review should acknowledge that reality. By comparing engineering documentation, manufacturing experience, testing discipline, and after-sales support, buyers can identify Hydraulic Cylinder Parts that perform reliably in real equipment, not just in a product photograph.
What Are the Best Hydraulic Cylinder Parts from China?

What Makes Hydraulic Cylinder Parts from China the Best Choice?

What Are the Best Hydraulic Cylinder Parts from China?

What Makes Hydraulic Cylinder Parts from China the Best Choice?

Chinese hydraulic cylinder parts can offer a practical balance between cost, capacity, and customization. Grand View Research estimates that the global hydraulic cylinders market reached about USD 14 billion in 2023. Demand is growing in construction, agriculture, material handling, and industrial equipment.

China supports this demand with extensive machining and metal-processing capacity. Experienced suppliers can produce piston rods, tube assemblies, seals, glands, and mounting components in varied specifications. Many factories also use CNC machining, induction hardening, honing, and pressure testing. These processes help control surface finish and dimensional accuracy. However, low price alone is not proof of quality.

The better choice depends on documented performance. Ask for material certificates, tolerance records, coating details, and test results. ISO 9001 certification can support process consistency, but it does not replace product inspection. The ISO 4413 standard also provides useful guidance for hydraulic system safety and component selection. According to MarketsandMarkets, automation and mobile machinery remain important growth areas for hydraulic equipment. Chinese suppliers serving these sectors may provide useful engineering support and shorter development cycles. Still, communication gaps can delay changes. That risk deserves attention.

Tips: Compare samples before bulk orders. Check rod straightness, seal compatibility, weld quality, and rated pressure. Request a third-party inspection when the application is critical. Keep a written approval record. Small details matter.

Which Hydraulic Cylinder Parts Are Commonly Manufactured in China?

What Are the Best Hydraulic Cylinder Parts from China?

Which Hydraulic Cylinder Parts Are Commonly Manufactured in China?

China commonly manufactures hydraulic cylinder tubes, piston rods, pistons, gland assemblies, end caps, mounting brackets, and seal carriers. These parts support construction equipment, agricultural machines, lifting systems, and industrial presses. Many factories produce standard sizes, but custom dimensions are also widely available.

Cylinder tubes often use honed steel surfaces for smoother sealing and longer service life. Piston rods may receive chrome plating, induction hardening, or corrosion-resistant treatment. Pistons are usually machined from steel or iron, depending on pressure and operating conditions. Seals, guide rings, and wipers are also produced in large volumes. Their material must match the fluid, temperature, pressure, and movement speed.

Quality depends on more than a low quotation. Buyers should review material certificates, dimensional reports, surface roughness records, and pressure-test results. A reliable manufacturer can explain tolerance limits without vague promises. Inspect bore diameter, rod straightness, thread accuracy, and weld penetration. Small errors can cause leakage or uneven movement.

No supplier gets every batch perfect. Even polished rods can show handling marks. This is where incoming inspection matters. I would request sample parts, test records, and clear drawings before approving production. A factory with traceable processes is usually safer than one offering only attractive pricing.

How to Evaluate Materials, Precision, and Manufacturing Quality

When evaluating hydraulic cylinder parts from China, start with the steel certificate, not the catalogue photograph. Ask for heat numbers, chemical composition, tensile strength, and impact results for every production batch. The World Steel Association reported 1.89 billion tonnes of crude steel production worldwide in 2023. Scale is not consistency. Material selection should match load, temperature, corrosion exposure, and fatigue cycles. For rods, verify surface-hardening depth and chrome thickness. For barrels, inspect honed finish and wall uniformity. Small omissions matter.

ISO 6020/2 and ISO 6022 define mounting and dimensional requirements, but buyers should request actual inspection records. Check bore diameter, rod straightness, concentricity, seal-groove dimensions, and surface roughness with calibrated instruments. A coordinate-measuring-machine report helps when linked to the serial number. In practical audits, random sampling can hide drift between batches. Compare first-piece and final-piece data. That habit catches gradual tool wear.

Manufacturing quality depends on heat-treatment control, welding qualification, cleaning, assembly discipline, and pressure testing. Request hardness maps, weld inspection results, cleanliness evidence, test pressure, hold time, and leakage records. The ISO Survey 2023 lists more than 1.2 million ISO 9001 certificates worldwide. Certification supports process control. It does not replace part-level evidence. A supplier may pass an audit and still miss a burr inside a port. That uncomfortable detail deserves inspection.

Which Standards and Tests Should Chinese Parts Meet?

When sourcing hydraulic cylinder parts from China, standards matter more than a polished catalogue. Reliable suppliers should provide traceable material certificates, controlled drawings, and documented inspection records. Steel, seals, rods, tubes, and pistons must match the approved specification.

Dimensional checks should cover bore diameter, rod diameter, thread accuracy, and seal-groove geometry. Surface roughness is critical. A rough chrome-plated rod can damage seals quickly. Suppliers should measure it with calibrated instruments, not visual judgment. Material certificates should follow EN 10204 3.1 or an equivalent documented system. Hardness testing and coating-thickness checks also deserve attention.

Pressure testing should include proof pressure, leakage inspection, and holding time. Fatigue testing is valuable for cylinders used on cranes, agricultural machines, or production lines. Cleanliness testing should follow a recognized method, such as ISO 4406 for hydraulic contamination control. Welding areas may need visual inspection, dimensional checks, and non-destructive testing.

Ask for calibration certificates. Ask for batch records. Keep samples.

ISO 9001 certification can support process control, but it does not prove every part is suitable. The actual test report must match the delivered batch. I have seen documents that looked complete but lacked test dates or operator signatures. That small gap matters. A practical audit should compare drawings, raw materials, inspection results, and packaging labels before shipment. Supplier experience helps, but independent verification remains the safer choice.

What Are the Best Hydraulic Cylinder Parts from China? - Which Standards and Tests Should Chinese Parts Meet?
Hydraulic Cylinder Part Key Quality Dimensions Relevant Standards and References Recommended Tests or Inspection Typical Acceptance Criteria
Cylinder Tube Material grade, internal diameter, wall thickness, straightness, internal surface finish, weld quality and corrosion protection. ISO 6020/1 or ISO 6020/2 for dimensional series where applicable; EN 10305-1 or ASTM A519 may be used for suitable precision steel tubes; ISO 286 for fits and tolerances. Dimensional inspection, material certificate review, ultrasonic or eddy-current testing when specified, internal roughness measurement and pressure testing of the completed cylinder. Dimensions match the approved drawing; no harmful laminations, cracks or leakage; internal roughness and straightness comply with the drawing or purchase specification.
Piston Rod Steel grade, yield strength, diameter, straightness, concentricity, surface hardness, chrome or alternative coating thickness and corrosion resistance. ISO 6020/1 and ISO 6020/2 for applicable cylinder dimensions; ISO 1302 for surface texture indication; ISO 21920 for profile surface texture; ISO 1461 may apply to hot-dip galvanized components, not hard-chrome plating. Hardness testing, coating-thickness measurement, visual inspection, roughness measurement, runout inspection, salt-spray testing when required by the coating specification and magnetic-particle testing for critical steel areas. No peeling, blistering, deep scratches or exposed base metal in functional areas; rod runout, hardness, coating thickness and roughness meet the approved drawing.
Piston Dimensional accuracy, sealing-groove geometry, material strength, wear resistance, concentricity and resistance to extrusion under pressure. ISO 286 for dimensional fits; ISO 3601 for O-ring groove and O-ring dimensions where O-rings are used; ISO 6020/1 or ISO 6020/2 for applicable cylinder series. CMM or calibrated dimensional inspection, groove inspection, hardness testing for metallic pistons and functional assembly testing with the specified seal set. Correct fit without binding; seal grooves are free of burrs; piston movement is smooth; no abnormal bypass leakage during pressure and endurance testing.
Cylinder Head and Cap Port dimensions, mounting interface, concentricity, sealing surfaces, thread quality, pressure resistance and corrosion protection. ISO 6020/1, ISO 6020/2 or ISO 6022 where applicable; ISO 4413 for hydraulic-system safety principles; ISO 7-1 or ISO 6149 may apply to specified pipe or port threads. Thread-gauge inspection, dimensional inspection, surface-finish inspection, proof-pressure testing and leakage testing after assembly. Ports and mounting features match the drawing; no casting or machining cracks; no permanent deformation or external leakage at the specified test pressure.
Piston and Rod Seals Compound compatibility, temperature range, pressure rating, extrusion resistance, friction, compression set and resistance to wear. ISO 3601 for O-rings; ISO 815-1 for compression set of elastomers; ISO 188 for accelerated aging; ISO 1817 for resistance of rubber to liquids; ISO 23936-2 may be relevant for thermoplastic materials in demanding fluid environments. Material identification, dimensional inspection, hardness testing, compression-set testing, fluid-compatibility testing and dynamic seal-life testing in the actual or equivalent hydraulic fluid. Correct compound and dimensions; no cuts, cracks, deformation or contamination; leakage and friction remain within the purchaser’s specified limits throughout testing.
Guide Rings and Wear Bands Bearing material, width, clearance, compressive strength, wear resistance and compatibility with the cylinder fluid and temperature. ISO 3601 may apply when O-rings are integrated into the design; ISO 23936-2 can be considered for thermoplastic material compatibility; final dimensions should be controlled by the approved drawing. Dimensional and visual inspection, material verification, compression or load testing and endurance testing under representative side-load conditions. No splitting, excessive wear, extrusion or seizure; installed clearance remains within design limits after endurance testing.
Rod Wiper and Scraper Seal Contaminant exclusion, wiping efficiency, lip geometry, low-temperature flexibility, wear resistance and compatibility with rod coating. ISO 3601 for associated O-rings where applicable; ISO 815-1, ISO 188 and ISO 1817 for elastomer performance; seal design dimensions should follow the approved technical drawing. Visual and dimensional inspection, low-temperature and fluid-compatibility testing, reciprocating wear testing and contamination-ingress testing. Wiper lip remains intact and properly seated; no unacceptable oil film, dirt ingress, tearing or hardening after the specified test cycles.
Tie Rods, Nuts and Fasteners Tensile strength, thread accuracy, preload retention, fatigue resistance, surface protection and resistance to loosening. ISO 898-1 for mechanical properties of carbon and alloy steel fasteners; ISO 965 for metric screw-thread tolerances; ISO 16047 for torque/clamp-force testing where required. Material certificate review, thread-gauge inspection, hardness testing, torque-preload verification, tensile testing and endurance testing of the assembled cylinder. Fastener property class and dimensions match the specification; threads are undamaged; torque and preload are controlled; no loosening or fracture during testing.
Welded Joints and Welded Attachments Joint strength, penetration, alignment, heat-affected-zone condition, porosity, cracking and distortion. ISO 3834 for quality requirements for fusion welding of metallic materials; ISO 5817 for quality levels of imperfections in fusion-welded joints; ISO 17635 for selection of non-destructive testing methods. Visual testing, dimensional inspection, magnetic-particle or dye-penetrant testing, ultrasonic testing or radiographic testing according to joint criticality and purchaser requirements. Weld quality meets the specified ISO 5817 quality level; no unacceptable cracks, lack of fusion, harmful porosity, distortion or pressure leakage.
Ports, Fittings and Mounting Interfaces Thread type, sealing method, pressure rating, dimensional interchangeability, orientation and resistance to vibration. ISO 1179 for ports and stud ends with ISO 228-1 threads; ISO 6149 for ports and stud ends with ISO 261 metric threads; ISO 8434 for selected metallic tube connections. Thread gauges, dimensional inspection, torque verification, pressure testing and vibration or endurance testing when required by the application. Correct thread and sealing configuration; fittings install without cross-threading; no leakage, cracking or rotation at the specified pressure and torque.
Complete Hydraulic Cylinder Assembly Rated pressure, proof pressure, leakage, force output, stroke accuracy, smoothness, cycle life, cleanliness and traceability. ISO 6020/1, ISO 6020/2 or ISO 6022 for applicable cylinder series; ISO 10100 for hydraulic fluid power cylinder acceptance tests; ISO 4413 for hydraulic-system safety principles; ISO 4406 for fluid cleanliness coding. Dimensional inspection, proof-pressure test, rated-pressure leakage test, functional stroke test, drift test, force test, endurance test, cleanliness inspection and final visual inspection. No unacceptable internal or external leakage, permanent deformation or abnormal noise; stroke, force, speed, drift and cycle-life results comply with the approved specification.
Manufacturing Documentation and Traceability Material traceability, revision control, inspection records, calibration status, nonconformance control and batch identification. ISO 9001 for quality-management systems; ISO 10012 for measurement-management systems; ISO 2859-1 may be used for attribute-based sampling inspection when an agreed sampling plan is established. Review of material certificates, inspection reports, calibration certificates, process records, nonconformance reports and final acceptance documents. Records are complete, legible and traceable to the production batch; measuring equipment is calibrated; deviations are documented and approved before shipment.
Important purchasing note: The exact pressure, leakage, dimensional tolerance, surface finish, coating thickness, cleanliness level and endurance requirements should be defined in the approved drawing and inspection plan. The standards listed above provide recognized technical references, but they do not replace application-specific engineering requirements or a mutually agreed acceptance specification.

How to Select a Reliable Chinese Hydraulic Cylinder Parts Supplier

What Are the Best Hydraulic Cylinder Parts from China?

How to Select a Reliable Chinese Hydraulic Cylinder Parts Supplier

China offers a wide range of cylinder tubes, piston rods, seals, pistons, and mounting parts. Grand View Research estimated the global hydraulic cylinders market at about USD 15.5 billion in 2023. This demand makes supplier selection more important, not easier.

Ask for material certificates, dimensional reports, and pressure-test records. A dependable supplier should identify steel grades, sealing materials, surface treatments, and production batches. Check whether its quality system follows ISO 9001 practices and whether products are designed around ISO 4413 safety principles. Do not accept vague claims. Request samples first.

Inspect a sample with calipers. Measure rod diameter, tube bore, thread depth, and mounting tolerances. Look for smooth chrome plating without pits or peeling. Seals should remain flexible after temperature and pressure testing. One overlooked detail can cause leakage.

Factory audits reveal more than polished catalogues. Review machining equipment, inspection tools, calibration dates, and nonconformance records. Ask how the supplier handles rejected parts. That answer matters.

Industry reports from MarketsandMarkets identify industrial automation and mobile equipment as major hydraulic demand areas. These applications need repeatable tolerances, not merely low prices. Compare total cost, including testing, packaging, replacement lead time, and rejected components. A cheaper piston may create expensive downtime.

Use a written specification and approval sample. Keep communication precise. Even experienced buyers sometimes miss seal compatibility or coating thickness. That mistake is worth admitting before mass production.

Hydraulic Cylinder Standard Working-Pressure Benchmarks

When selecting hydraulic cylinder parts from China, compare tubes, rods, seals, guides, and piston assemblies against the pressure class required by the cylinder design. These nominal benchmarks from ISO hydraulic cylinder series provide a practical starting point for checking supplier drawings, material certificates, dimensional tolerances, and pressure-test records.

A reliable supplier should clearly identify the applicable standard, rated pressure, sealing system, surface treatment, inspection method, and traceability documents for every critical part.